Manufacturing a fruit juice machine begins with the intended fruit, product flow, cleaning method, operating conditions and required output. Design and fabrication influence each other: dimensions, tolerances, surface finish and access for inspection must be specified before a suitable process can be selected. The same function can be achieved with different components, but each option must be checked against performance, sanitation, maintenance and cost requirements.
Material and production volume affect whether a component is machined, cast, forged, formed from sheet or made by another method. Geometry, required accuracy, available tooling and batch size also matter. No process is automatically the cheapest or most accurate for every part; compare feasible routes against the drawing and expected production quantity.
Choose joining methods for the actual load, material, cleaning needs and disassembly requirements. Welded, bolted and other joints have different fabrication and maintenance implications. For parts that contact juice, consider whether seams and crevices can be cleaned effectively; a change from welding to a threaded joint requires a design review rather than a simple substitution.
Delivery time can influence the fabrication plan, but a faster process is useful only if the finished part still meets its material, dimensional, strength and hygiene specifications. Document any design or process change and inspect the resulting part before assembly.
Cold forming can alter a material's mechanical properties. The result depends on the alloy, amount of deformation and later processing, so the required properties should be confirmed from material data and, where needed, testing. Do not assume that a particular forming step always increases strength or is suitable for a food-contact component.
Heat treatment can also change hardness and strength, but its effect depends on the material, temperature cycle, section size and target property. It does not universally double strength. Specify the required condition and verify it with appropriate inspection or testing rather than using a generic performance multiplier.
Turning, milling, drilling, boring and grinding may be combined to make a part. Select operations according to geometry, tolerances, surface finish and accessibility, then inspect critical dimensions and surfaces. A nominally precise process cannot compensate for an unsuitable drawing or uncontrolled setup.
In repeated production, tool wear, cutting conditions and chip removal affect consistency and surface quality. Plan for inspection and cleaning after machining so that metal fragments, burrs and residues do not remain in areas that may contact product.
Assembly should allow the machine to be installed, cleaned, adjusted and maintained. Removable connections can help access where appropriate, while permanent joints may be chosen for other functions. Review alignment, seals, guards and access points as a complete system rather than treating each component in isolation.
Finishing and coating choices depend on the location of the surface, the juice and cleaning agents it will encounter, and applicable market requirements. A decorative finish is not automatically suitable for food contact. For U.S. food-processing equipment, 21 CFR 117.40 addresses cleanable construction, corrosion-resistant food-contact surfaces, seams and prevention of contamination. Confirm the corresponding requirements for the destination market and the actual process.
- Fruit Juice Production Line
- Citrus Juice Processing Line
- Mango juice production line
- Apple Juice Processing Line
- Pineapple Juice Processing Line
- Pomegranate juice processing line
- Lychee juice processing plant
- Grape Juice Processing Line
- Full Automatic Milk Processing Plant
- Plant Protein Beverage Production Line
- Coconut Water Processing Line
- Industrial Coconut Milk Processing Line and Extraction Equipment
- Fruit Crusher Machine
- Tubular Fruit Preheater
- Steam Jacketed Kettle
- Fruit Belt Press Filter
- Spiral Juice Extractor
- Fruit Peeling and Squeezing Machine
- Citrus Fruits Peel Essential Oil Extractor
- Double Screw Extractor for Grape
- Fruit Pulping Machine
- Mango Peeling and Destoning Machine
- Grape Destemmer Crusher
- Automatic Coconut Cutting Machine
- Tender Coconut Half Cutting Machine
- grape wine squeezing machine
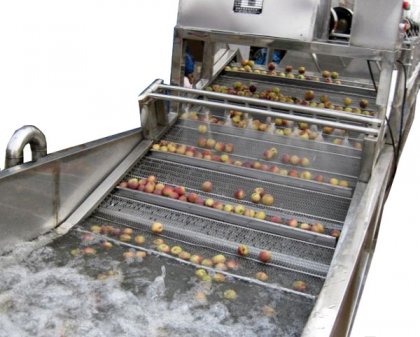

Compare four industrial fruit washing machine types and AGICO bubble washer models. Select by capacity, cleaning action, materials and fruit handling....
Follow six industrial mango juice processing steps, from sorting and pulping to blending, heat treatment, filling and cooling. See equipment choices and figures to confirm....
Compare gravity, pressure, vacuum, flow-meter and weighing juice filling machines. Learn how beverage type, bottle, capacity and cleaning needs guide selection....